
GD&T symbols turn a drawing from a list of sizes into a controlled description of how machined features relate to one another. The most useful symbols for CNC parts are position, flatness, perpendicularity, parallelism, profile, concentricity, and runout, but each controls a different condition and needs an appropriate datum or inspection method. Use GD&T when function, fit, sealing, rotation, or assembly depends on feature relationships; do not add tight geometric tolerances simply to make a drawing look precise.
What GD&T Symbols Communicate
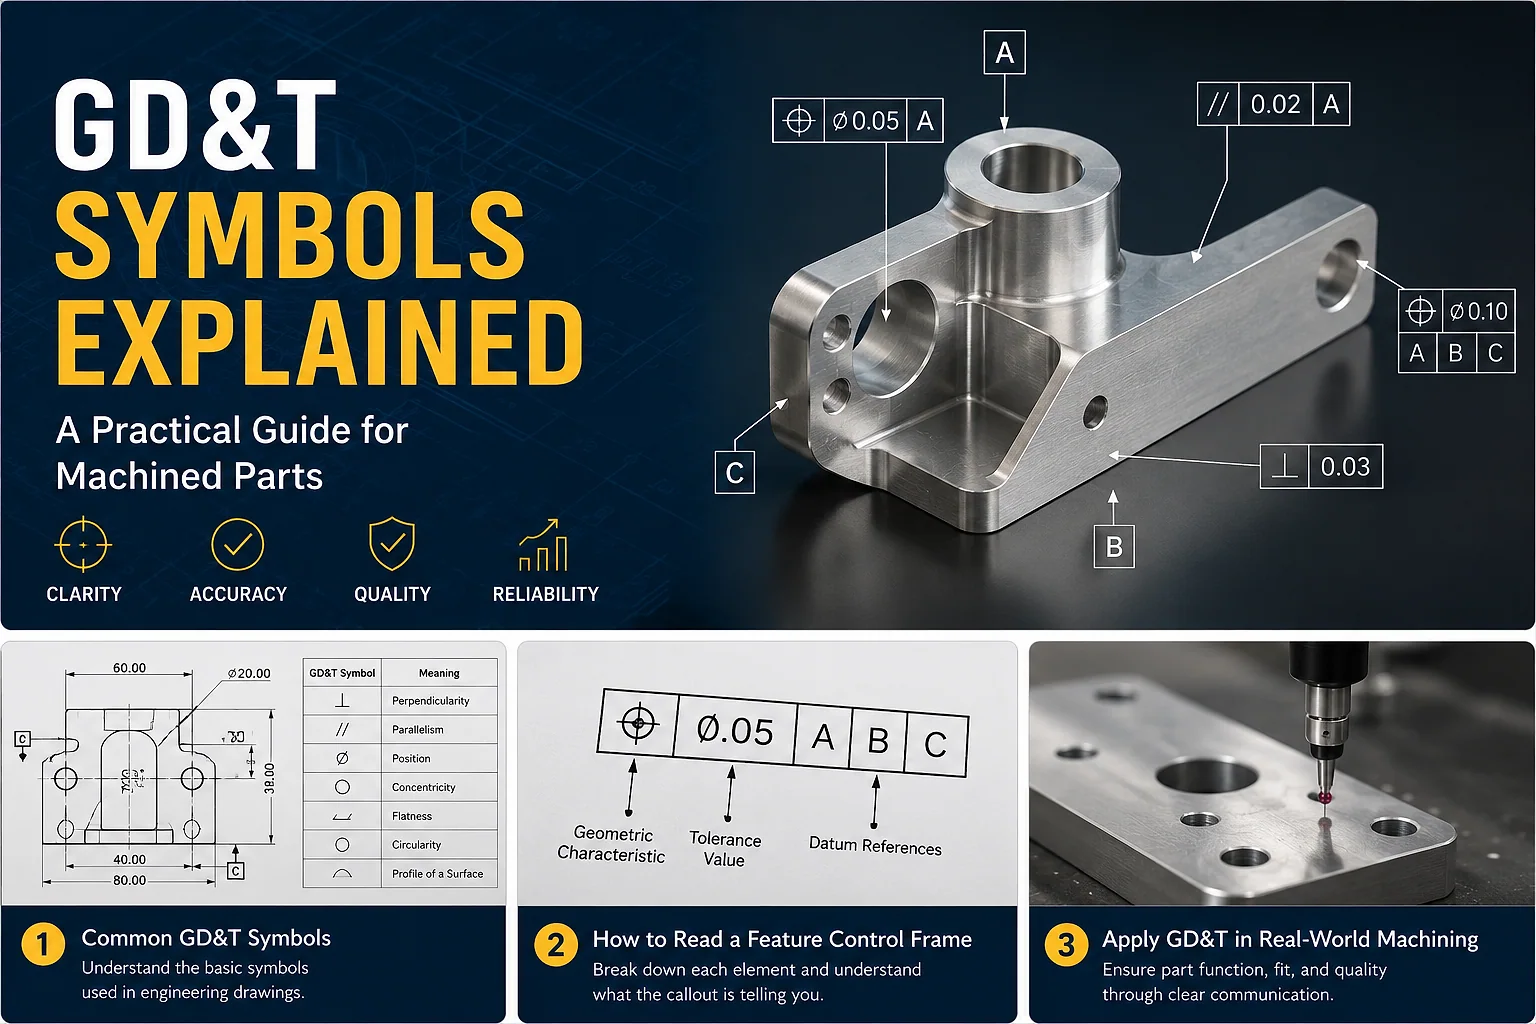
Geometric Dimensioning and Tolerancing (GD&T) uses standardized symbols, tolerance values, datum references, and modifiers to control form, orientation, location, and runout. A feature control frame commonly contains a geometric characteristic symbol, a tolerance zone, and one or more datum references. Together, these elements tell the manufacturer what must be controlled and tell the inspector how to evaluate it.
Size tolerances answer “how large?” GD&T answers questions such as “how flat?”, “how square to datum A?”, “how accurately located from A, B, and C?”, or “how much may this surface vary as the part rotates?” The distinction matters because two parts can share the same hole diameter yet assemble differently if their hole positions or datum relationships vary.
For a practical inspection perspective, see what buyers should check in a CMM report.
Datums: The Reference Framework
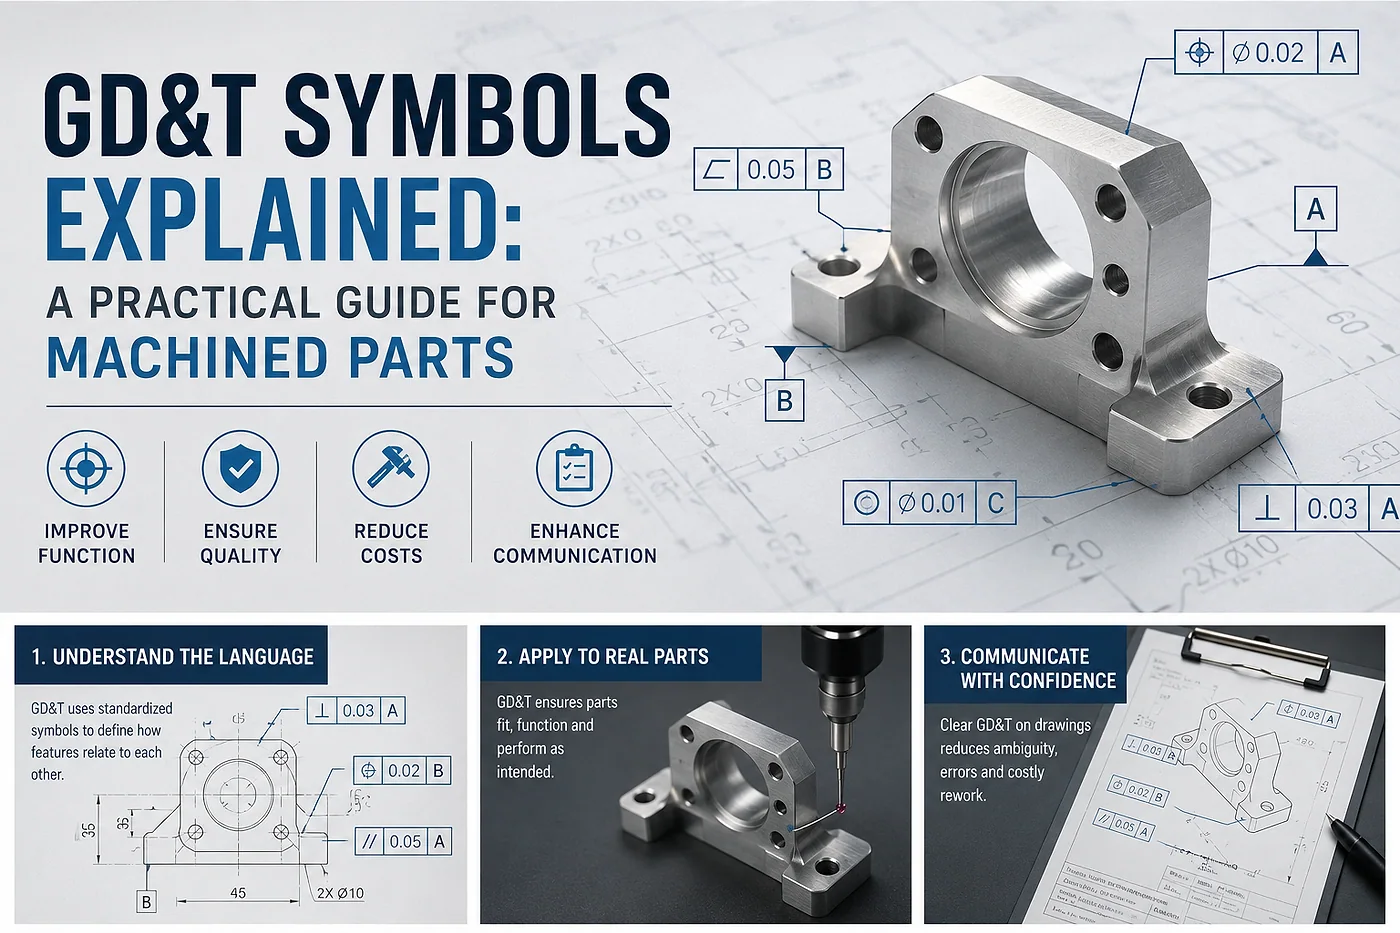
A datum is a theoretically exact reference derived from a physical surface, axis, or center plane. Datum A is commonly the primary mounting face, B a perpendicular side or axis, and C a third feature that prevents the remaining movement. The order matters: changing the datum sequence can change the functional meaning of a position or orientation tolerance.
Choose datums from the way the part is assembled, supported, located, or measured. A convenient outside edge may be easy to probe but may not represent the interface that controls performance. Datum targets may be preferable for cast, rough, or flexible surfaces where the entire surface cannot establish a stable reference.
- Use the primary datum to represent the main mounting or seating condition.
- Use the secondary datum to control rotation or a key perpendicular relationship.
- Use the tertiary datum to locate the final degree of freedom.
- Keep datum surfaces large, stable, and accessible to workholding and inspection.
- Confirm that the inspection setup reproduces the assembly datum simulator.
Common GD&T Symbols Explained
| Symbol name | What it controls | Typical machined-part use | Common inspection approach |
|---|---|---|---|
| Flatness | Surface form without a datum | Mounting face, seal land, plate | CMM, surface plate, height scan |
| Parallelism | Orientation relative to a datum | Opposing faces, guide surfaces | CMM or height variation from datum |
| Perpendicularity | 90-degree orientation to a datum | Bore axis, shoulder, bracket wall | CMM, square datum setup, gauge |
| Position | Feature location and orientation | Hole patterns, pins, bolt circles | CMM, functional gauge, vision |
| Profile of a surface | 3D surface boundary | Cast transitions, contoured housings | CMM scan or optical comparison |
| Circular runout | Radial variation at one section as part rotates | Turned diameters, bearing seats | Indicator while rotating datum axis |
| Total runout | Full-surface variation as part rotates | Precision cylinders and faces | CMM or indicator sweep during rotation |
The table is a selection guide, not a complete standard. Symbol interpretation also depends on the tolerance zone shape, datum order, material condition modifiers, and the drawing standard referenced by the project.
Form Controls: Flatness, Straightness, Circularity, and Cylindricity
Form controls describe the shape of an individual feature and normally do not reference a datum. Flatness limits all points on a surface to a pair of parallel planes. It is useful for a sealing face or mounting plate when orientation to another feature is not the issue. Straightness can control a line element or an axis, while circularity limits each circular cross-section.
Cylindricity controls the entire cylindrical surface with a coaxial tolerance zone. It can be powerful but expensive to inspect and may be unnecessary when separate size, straightness, and runout controls already protect function. Select the least complex control that fully describes the engineering need.
Orientation Controls: Parallelism and Perpendicularity
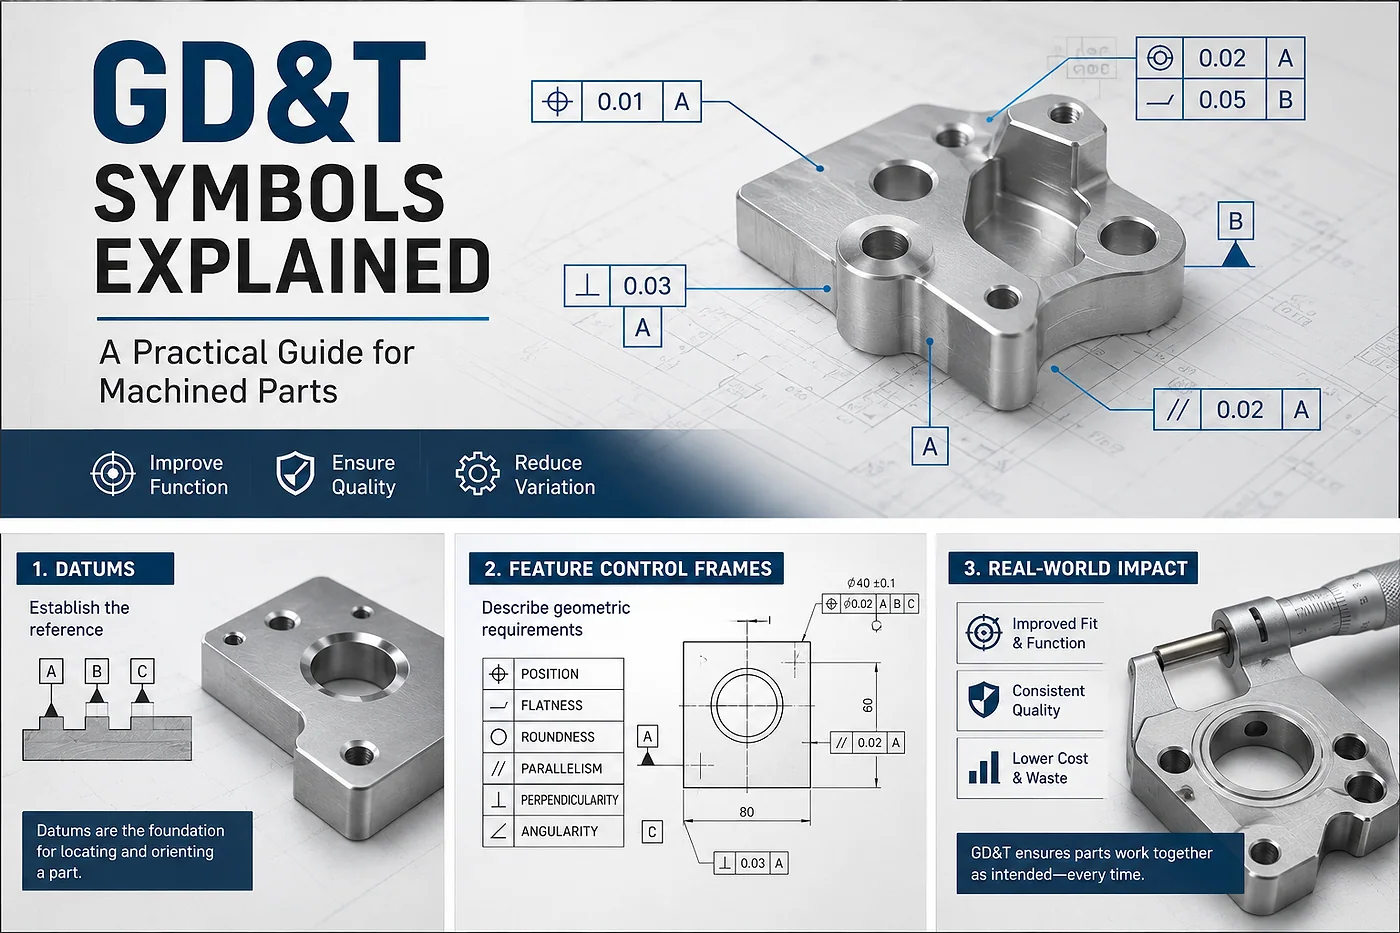
Parallelism controls the orientation of a surface, line, or axis relative to a datum. Perpendicularity controls a 90-degree relationship. Neither symbol automatically controls feature location unless the callout and datum scheme make location functionally constrained.
For a machined bracket, perpendicularity may keep a wall square to the mounting face so a mating plate seats correctly. For a guide plate, parallelism may control the relationship between two rails. If the real requirement is the location of a hole axis, position is usually more direct than combining multiple orientation notes.
Our guide to CNC machined brackets and hole position shows how datum faces and hole patterns work together in production.
Location Controls: Position and Profile
Position is the primary GD&T control for locating holes, pins, slots, and bosses from a datum reference frame. A cylindrical position zone controls the feature axis and, when applied correctly, allows the inspector to evaluate the entire pattern rather than checking unrelated plus/minus dimensions. Bonus tolerance may apply when a material condition modifier is specified.
Profile of a surface controls a 3D boundary around a contoured surface. It is useful for blended housings, cast transitions, aerodynamic forms, and machined surfaces where size dimensions alone cannot define the shape. Profile may reference datums when the surface must be located and oriented, or it may be used as a form control.
A position callout such as a diameter 0.02 mm tolerance to datums A, B, and C is not interchangeable with a coordinate dimension of +/-0.01 mm. The tolerance zone, datum mobility, and inspection method are different. State the applicable standard and modifiers so the supplier does not have to infer intent.
Runout and Rotational Features
Circular runout limits variation at each circular section as a part rotates around a datum axis. Total runout evaluates the entire surface while rotating, controlling cumulative variation along the feature. Runout is commonly applied to bearing seats, shafts, hubs, sealing diameters, and turned faces.
Runout requires a realistic datum axis and a repeatable rotational setup. If the datum bore is rough, contaminated, or not functionally representative, the measurement may describe the inspection fixture rather than the assembly condition. Clean the datum, control support, and record indicator direction and rotation speed where the requirement is critical.
For bearing interfaces, see bearing-seat bore, shoulder, and runout guidance.
Reading a Feature Control Frame
- Read the geometric characteristic symbol in the first compartment.
- Read the tolerance value and identify whether the zone is diametrical, linear, projected, or otherwise modified.
- Read datum references in their order of precedence.
- Check material condition modifiers such as MMC or LMC and any datum modifiers.
- Follow the leader to the controlled feature and confirm whether the callout applies to a surface, axis, pattern, or derived median line.
- Confirm the size dimension and basic dimensions that locate the true position.
Do not interpret the frame in isolation. A position tolerance depends on basic dimensions and datums, while a flatness tolerance may stand alone. Notes about all-around, statistical tolerancing, tangent plane, or unequal distribution can change the inspection result.
Applying GD&T to CNC Process Planning
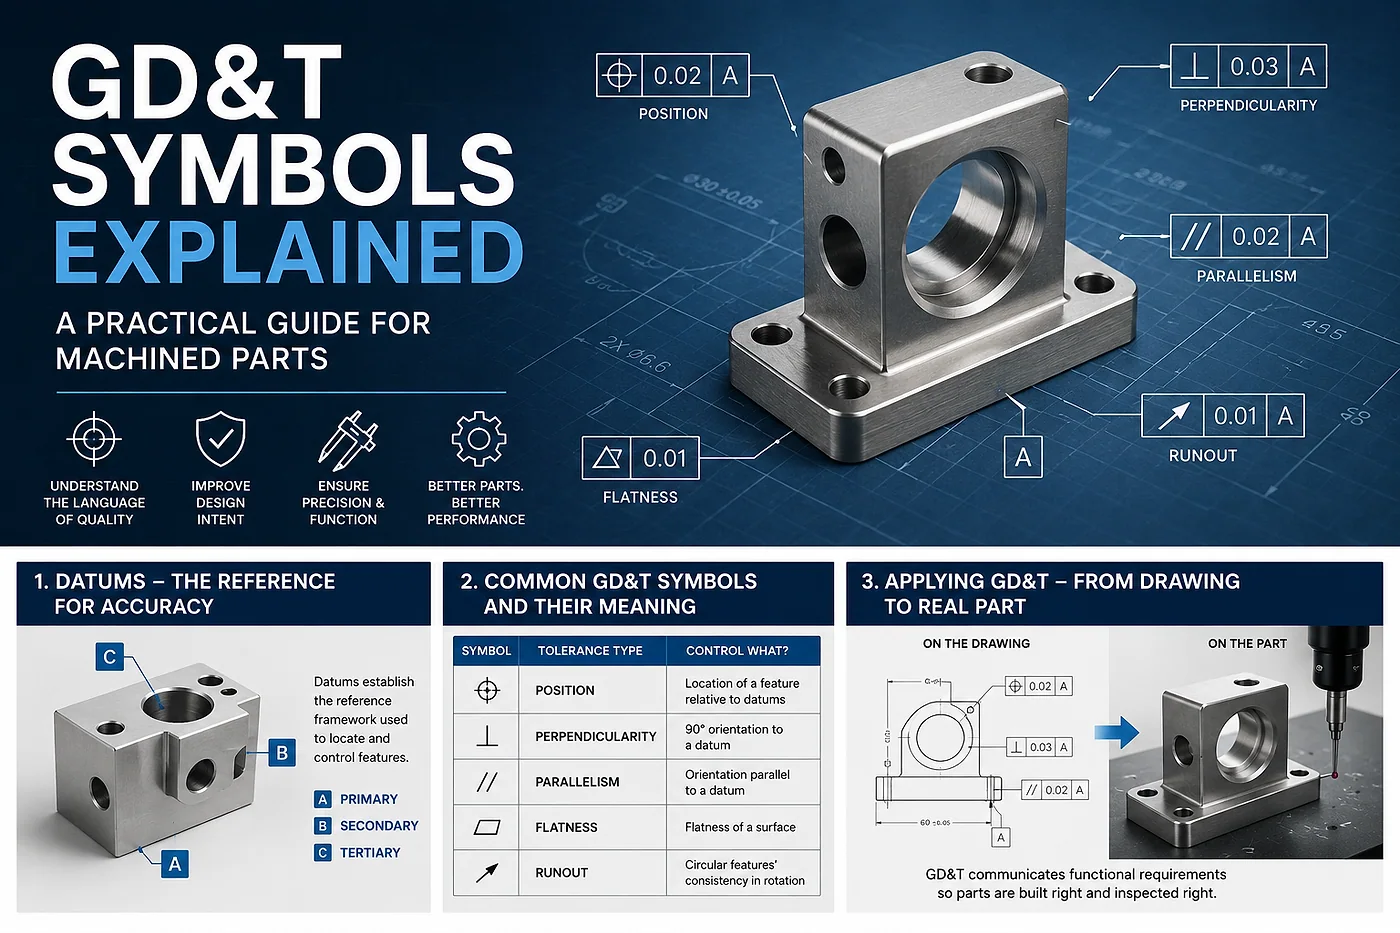
Manufacturing should plan the setup sequence around the datum structure. Machine the primary datum first when practical, establish secondary and tertiary references in stable setups, and avoid re-clamping in a way that loses the functional relationship. Probe or qualify work offsets from the same references used for inspection.
Tool access, cutter deflection, thermal growth, burrs, stock stress, and surface treatment can all affect geometric results. A position tolerance on a deep hole may require a rigid drilling or boring strategy. A flatness requirement on a thin plate may need stress-relieved stock, balanced roughing, and a final light pass. A perpendicularity requirement on a welded assembly may be controlled after welding rather than after the initial cut.
- Translate each critical frame into a process feature, setup reference, and measurement method.
- Reserve machining allowance for faces or bores that must be finished after distortion-producing operations.
- Measure datums before using them to locate downstream features.
- Inspect after anodizing, plating, passivation, or blasting when the finish can change the requirement.
- Use first article inspection to prove the complete datum and feature-control scheme.
Inspection Methods and Supplier Communication
A CMM is useful for position, profile, perpendicularity, parallelism, and datum-related relationships. Micrometers, bore gauges, air gauges, indicators, surface plates, optical comparators, and functional gauges each have a place. The selected instrument should resolve the tolerance and reproduce the functional datum setup.
Ask suppliers to identify the drawing standard, inspection temperature, datum fixtures, probe strategy, calibration status, and whether results are reported as actual values or pass/fail. A CMM report without a clear datum alignment can look detailed while failing to prove the intended requirement.
For broader drawing and tolerance review, see common CNC tolerance problems that begin before cutting.
Designing Clear GD&T Callouts
- Start with the assembly function and identify the surfaces or axes that actually locate the part.
- Use basic dimensions for theoretically exact locations controlled by GD&T.
- Apply the least restrictive tolerance that protects fit, sealing, motion, or performance.
- Avoid stacking several controls that duplicate the same requirement or create an unintended conflict.
- Define the finished condition when coating, heat treatment, or finishing affects size or geometry.
- Show datum feature symbols on accessible, stable surfaces and make inspection feasible.
- Call out pattern requirements and composite tolerances when hole-to-hole relationships matter.
Related DAXIN Services
DAXIN supports DFM review, CNC milling and turning, datum-based process planning, CMM inspection, first article inspection, tolerance analysis, surface finishing coordination, and batch production of parts defined with GD&T.
FAQs
1. What are GD&T symbols?
GD&T symbols are standardized drawing symbols that control feature form, orientation, location, profile, and runout in relation to specified tolerances and datums.
2. Which GD&T symbol is used for hole location?
Position is normally used to control the location and orientation of holes, pins, slots, and bosses from a datum reference frame.
3. Does flatness require a datum?
No. Flatness is a form control that limits a surface between two parallel planes without referencing a datum.
4. What is the difference between perpendicularity and position?
Perpendicularity controls 90-degree orientation to a datum. Position controls a feature’s location and orientation within a defined tolerance zone.
5. When should a drawing use profile of a surface?
Use profile when a 3D contour, blended transition, or complex surface boundary must be controlled more completely than individual size dimensions can provide.
6. What do datum references A, B, and C mean?
They identify the ordered primary, secondary, and tertiary references that establish the coordinate frame for locating and orienting controlled features.
7. How is runout inspected?
Runout is commonly checked by rotating the part around a qualified datum axis and measuring variation with an indicator or CMM.
8. Can GD&T reduce machining cost?
Yes. Functional tolerancing can prevent unnecessarily tight size limits and focus inspection on features that affect assembly, although complex or very tight geometric controls may increase cost.
9. Does a CMM automatically prove every GD&T callout?
No. The CMM must use the correct datum alignment, probe strategy, feature definition, temperature control, and drawing standard for the specific callout.
10. What should a supplier receive with a GD&T drawing?
Provide the current drawing standard, 3D model, revision, material and finish, datum intent, critical assembly interfaces, inspection requirements, and any first article or traceability expectations.
Final Thoughts
GD&T symbols are most useful when they express real assembly and inspection requirements. Select datums from the functional interfaces, use position for feature location, orientation controls for relationships, flatness for independent surface form, and runout for rotating features. Clear callouts let the CNC team plan stable setups and let the inspector produce evidence that the part will work as intended.
Request a GD&T Drawing Review
Send your drawing, 3D model, critical interfaces, material, finish, and inspection goals to DAXIN CNC for a GD&T and CNC manufacturability review.